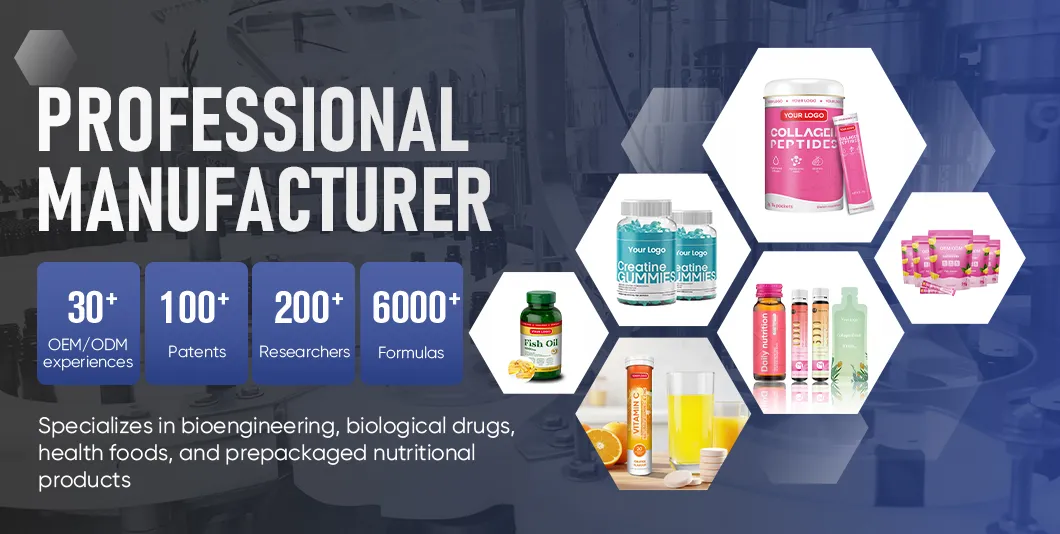
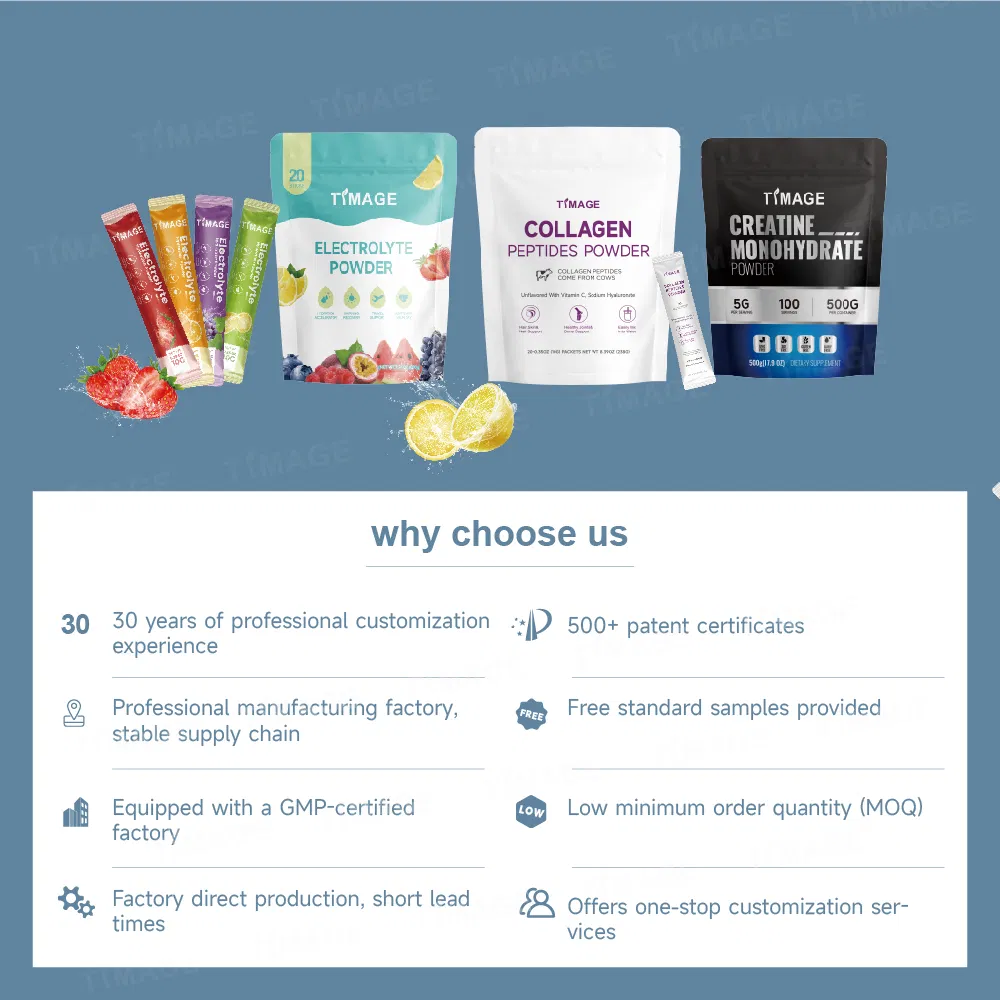
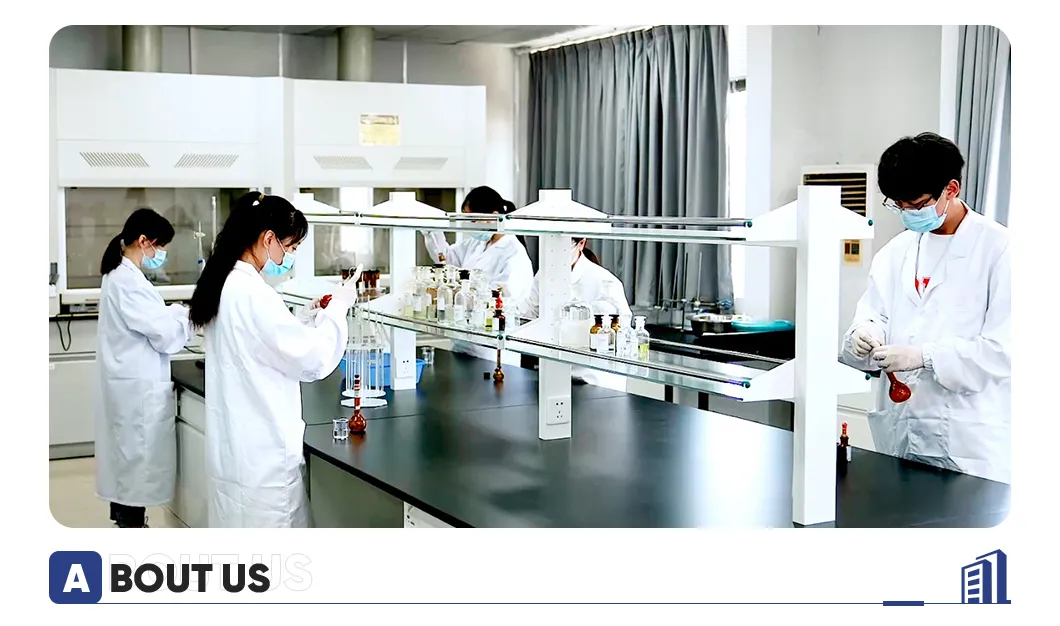
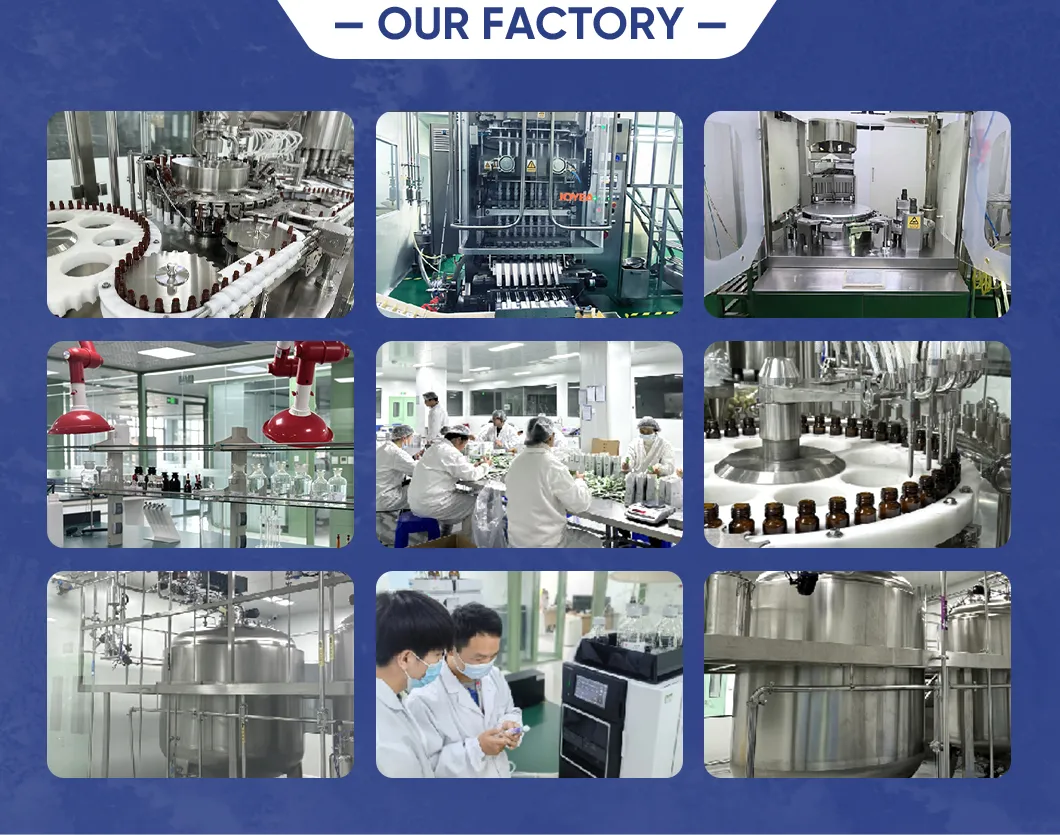
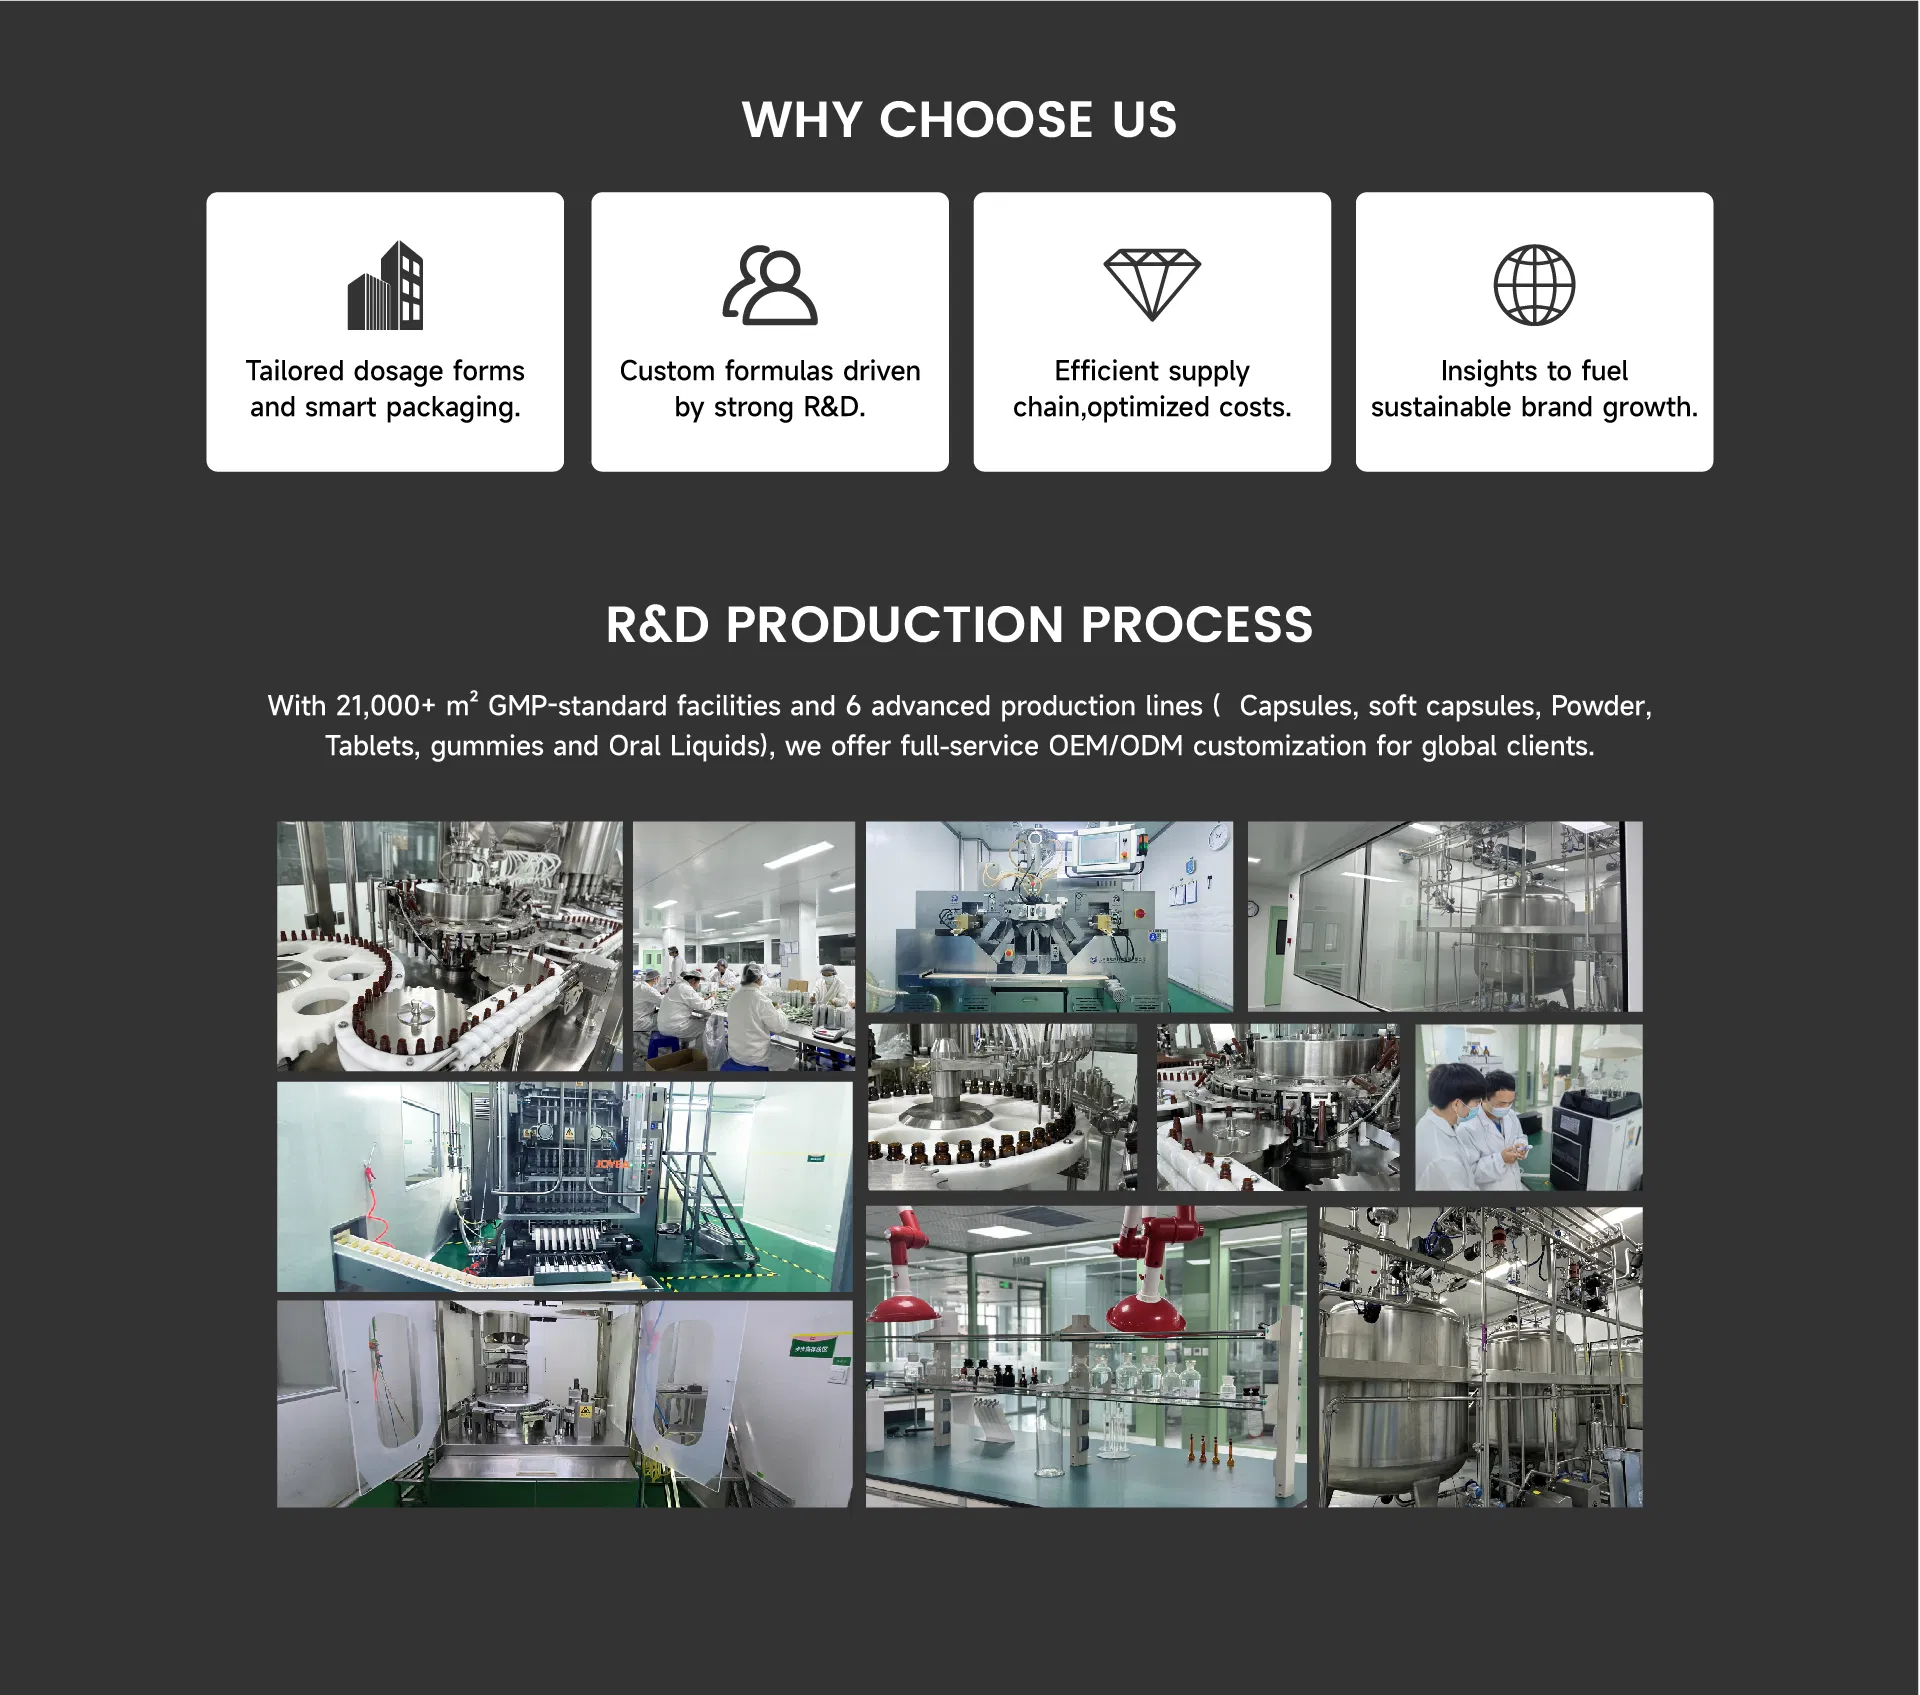
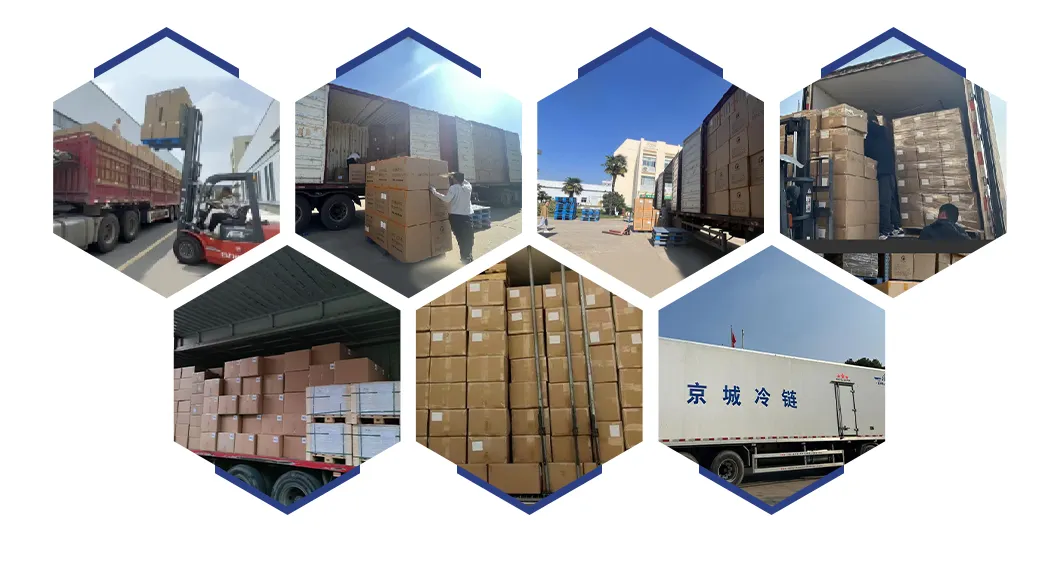
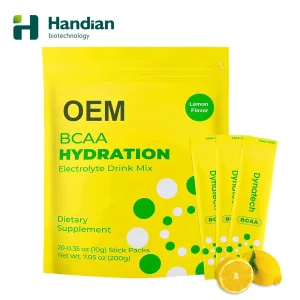
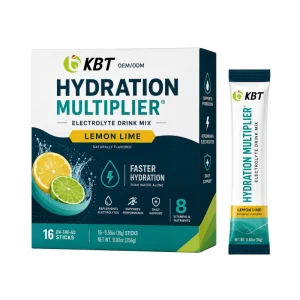
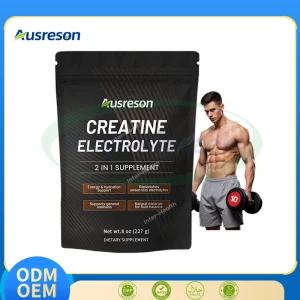
We are a combined enterprise specializing in bioengineering, biological drugs, health foods, and prepackaged nutritional products. With a total land area of 21,138 square meters, we operate with strong in-house manufacturing capabilities. The company runs multiple health care production lines, supporting daily capacities of up to several million units through advanced equipment such as mixing machines, ingredient tanks, sterilization machines, tablet machines, automatic bottling machines, granulators, dryers, and filling machines.
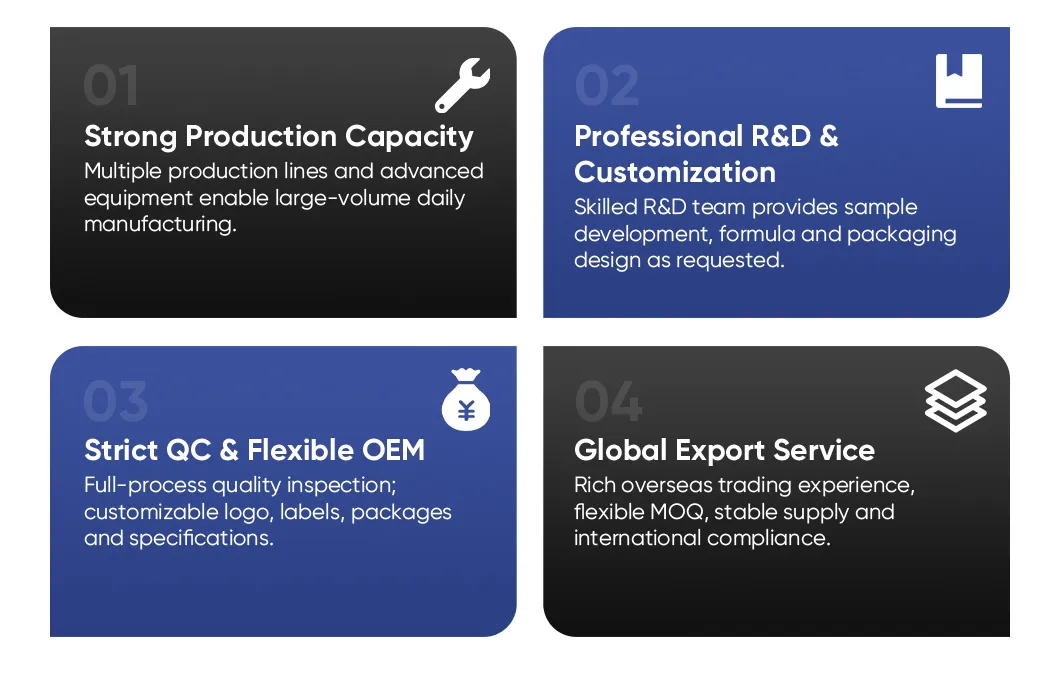
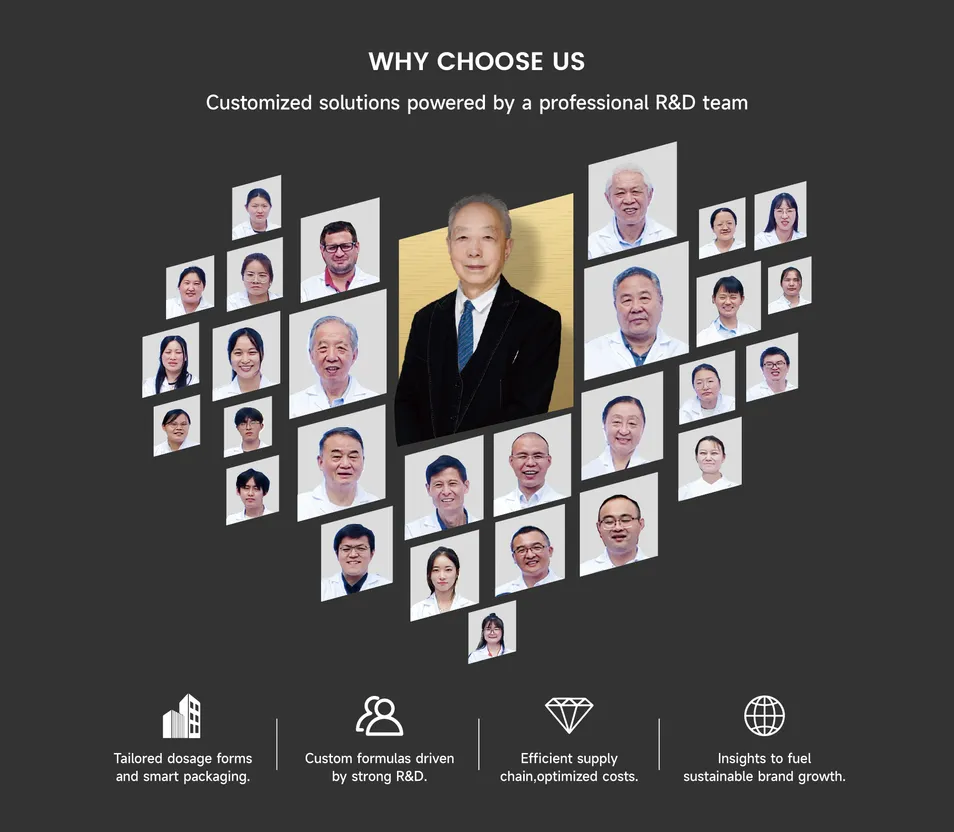
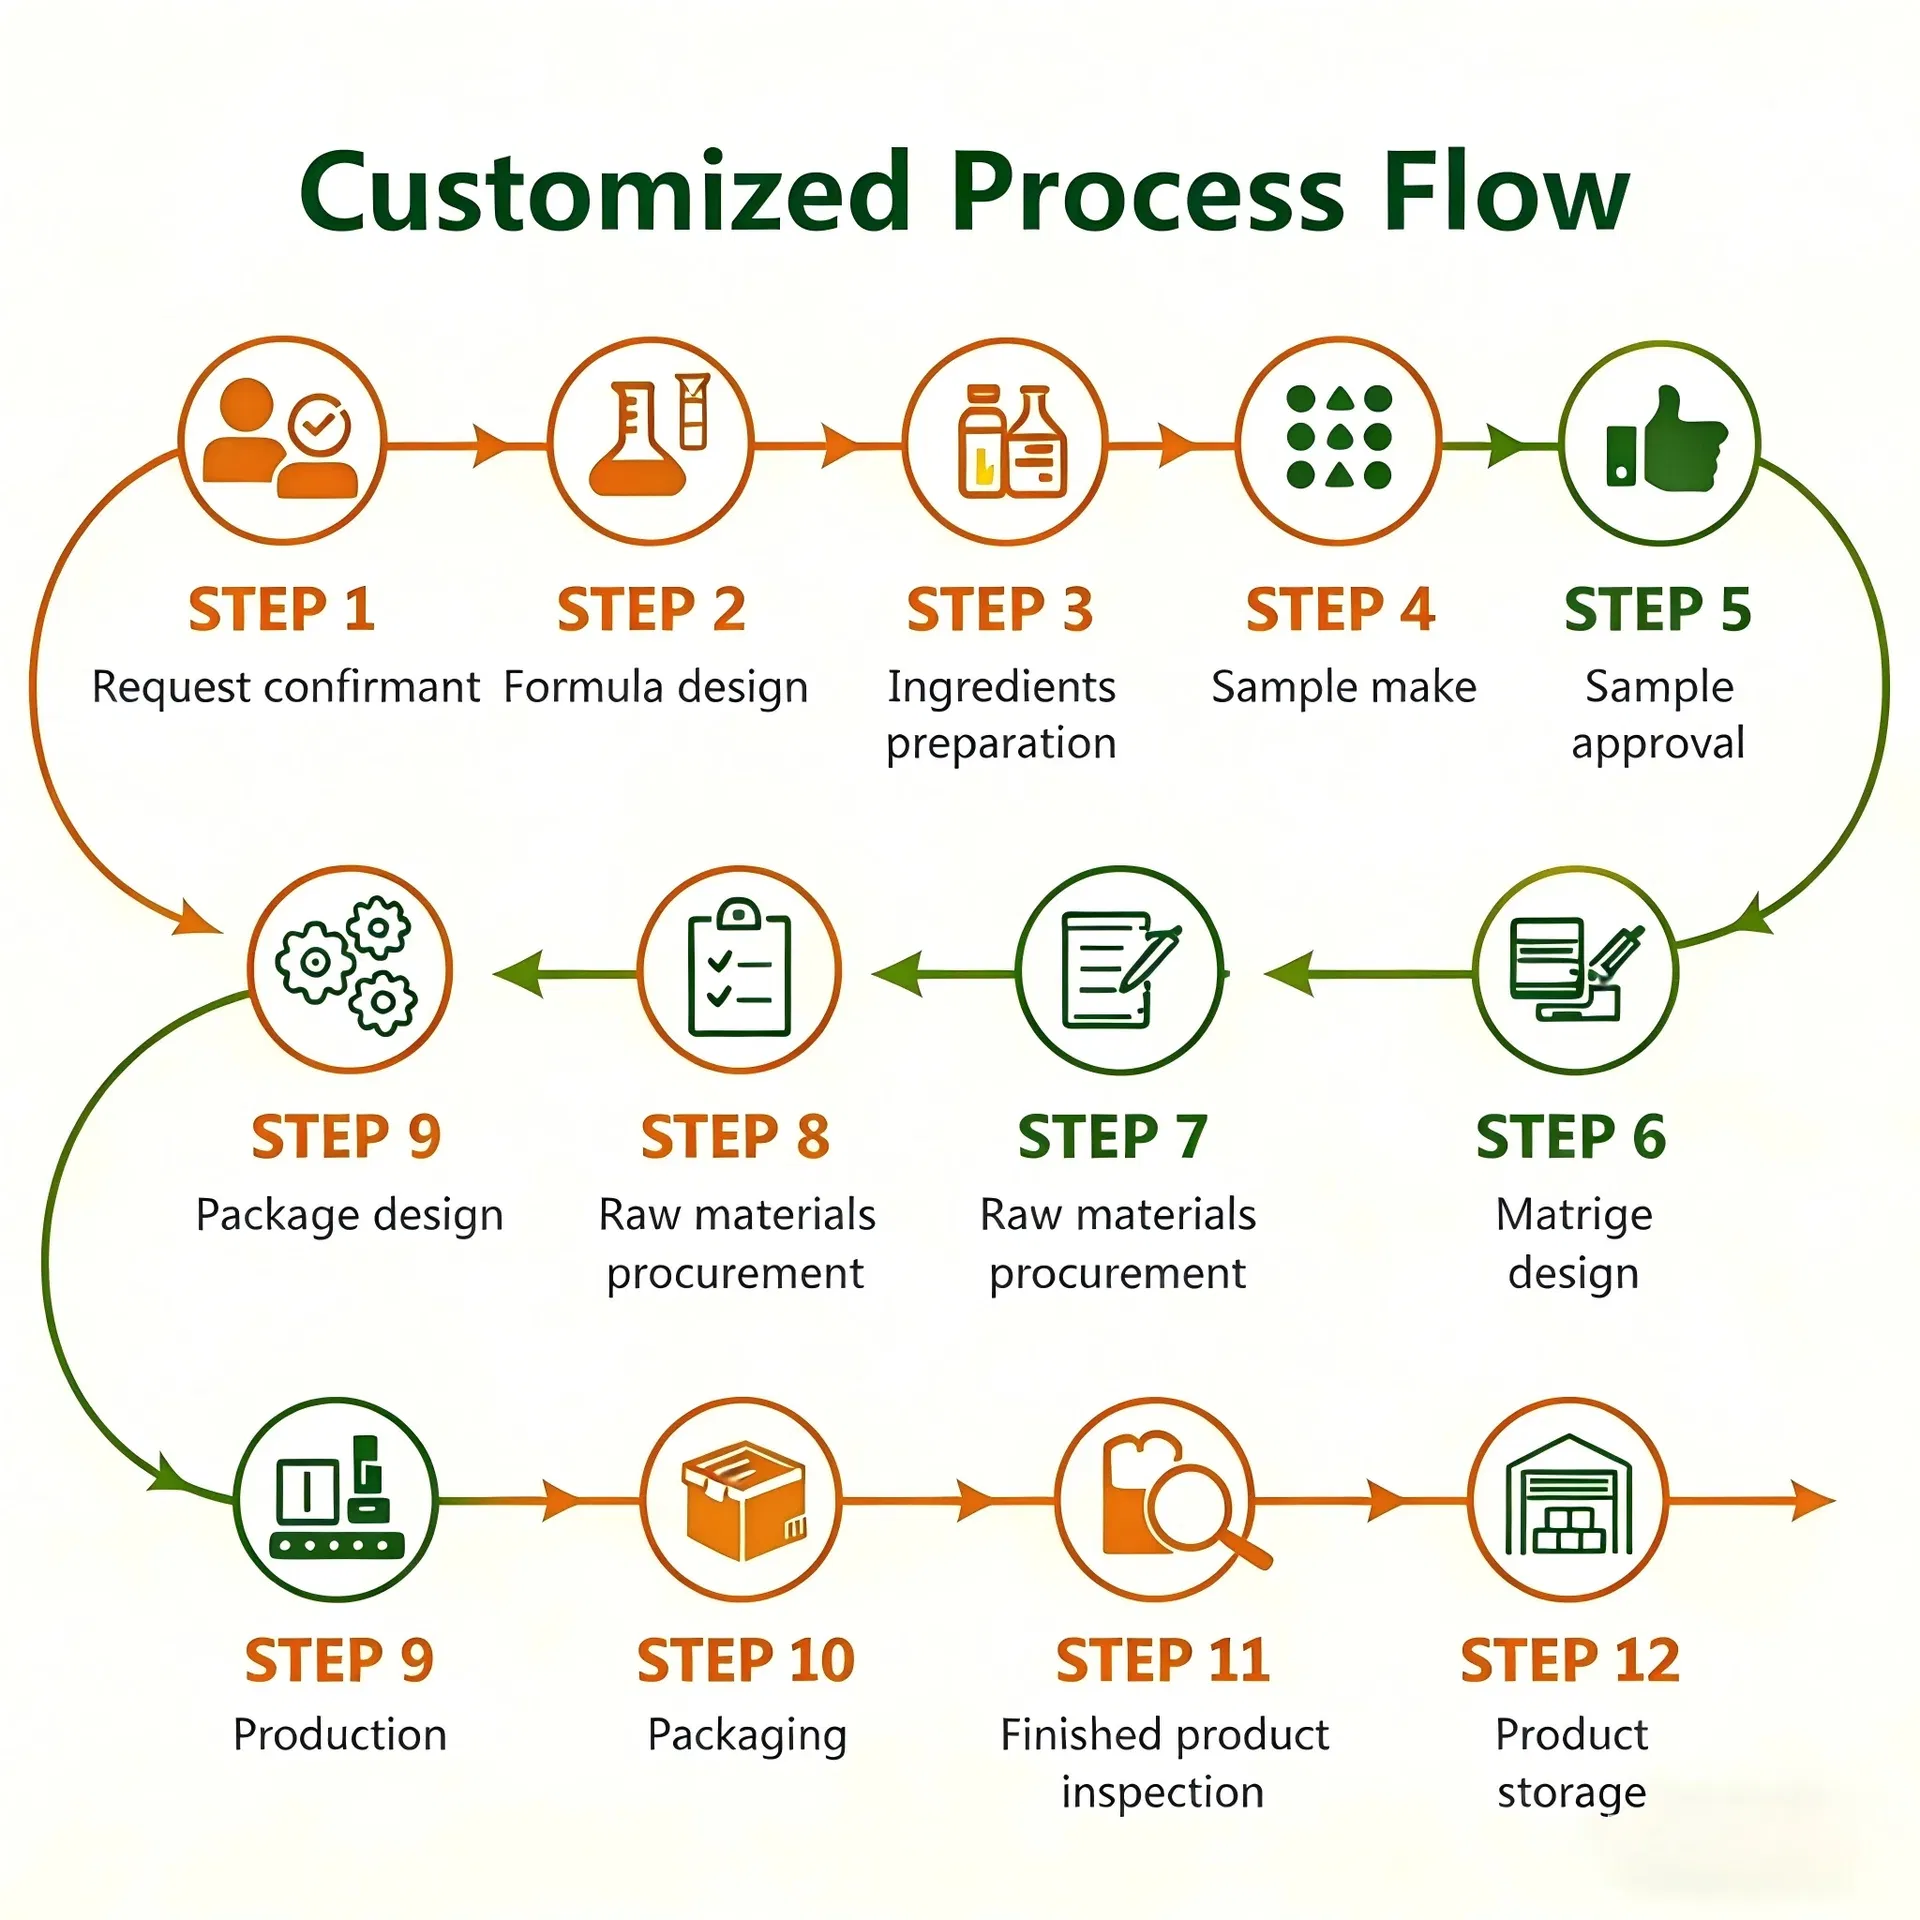
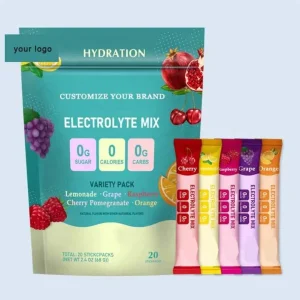
Our professional workforce of 237 employees includes 14 experienced R and D engineers, among them 10 post-graduate researchers dedicated to bioengineering and nutritional formulation innovation. New samples and product concepts can be processed and customized on demand, supported by services like sample processing and graphic processing to match client branding. To ensure stable quality, 32 QA QC inspectors oversee every production stage, while flexible customization options for logo, label, packaging, color, size, graphic design, and material replacement help meet diverse engineering and formulation requirements.
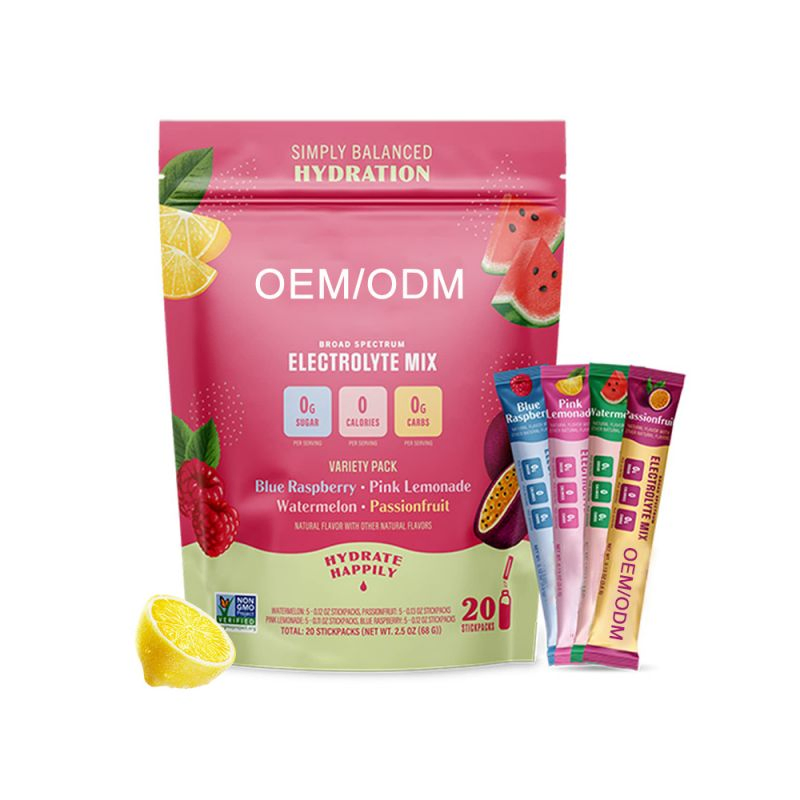
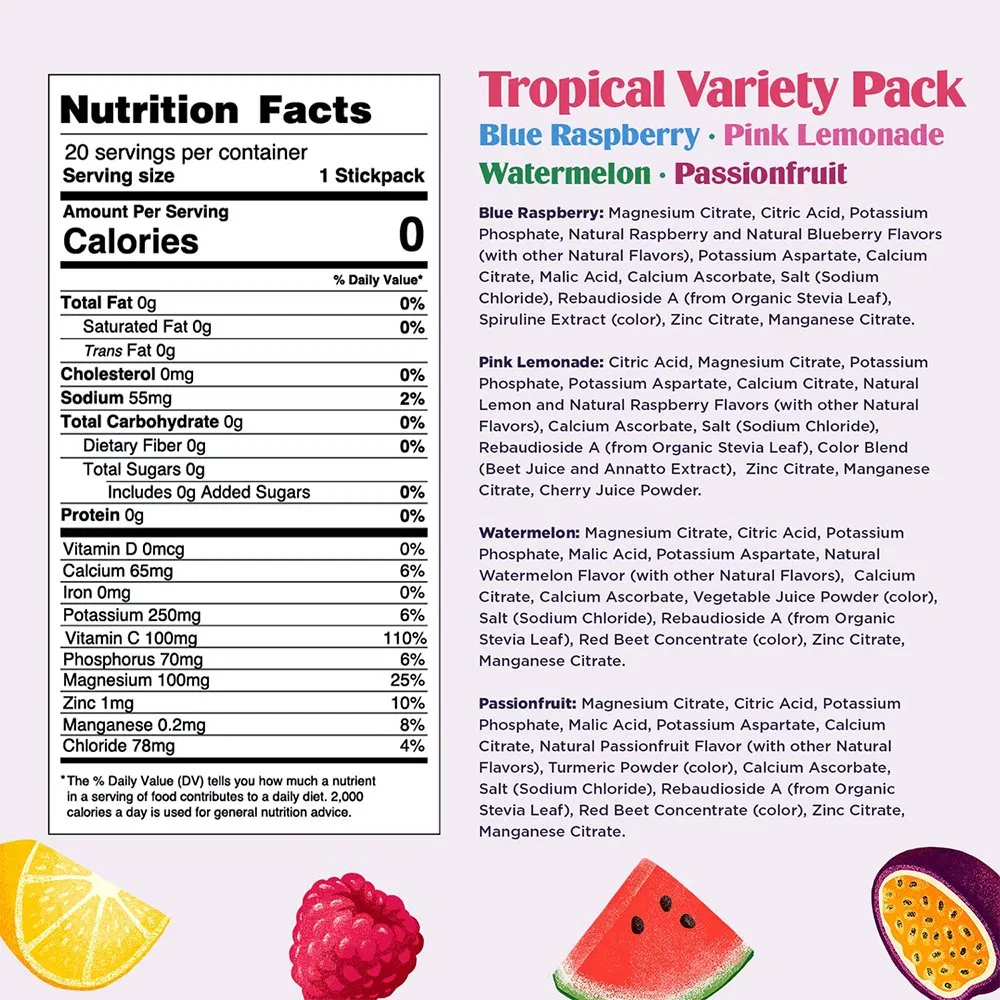
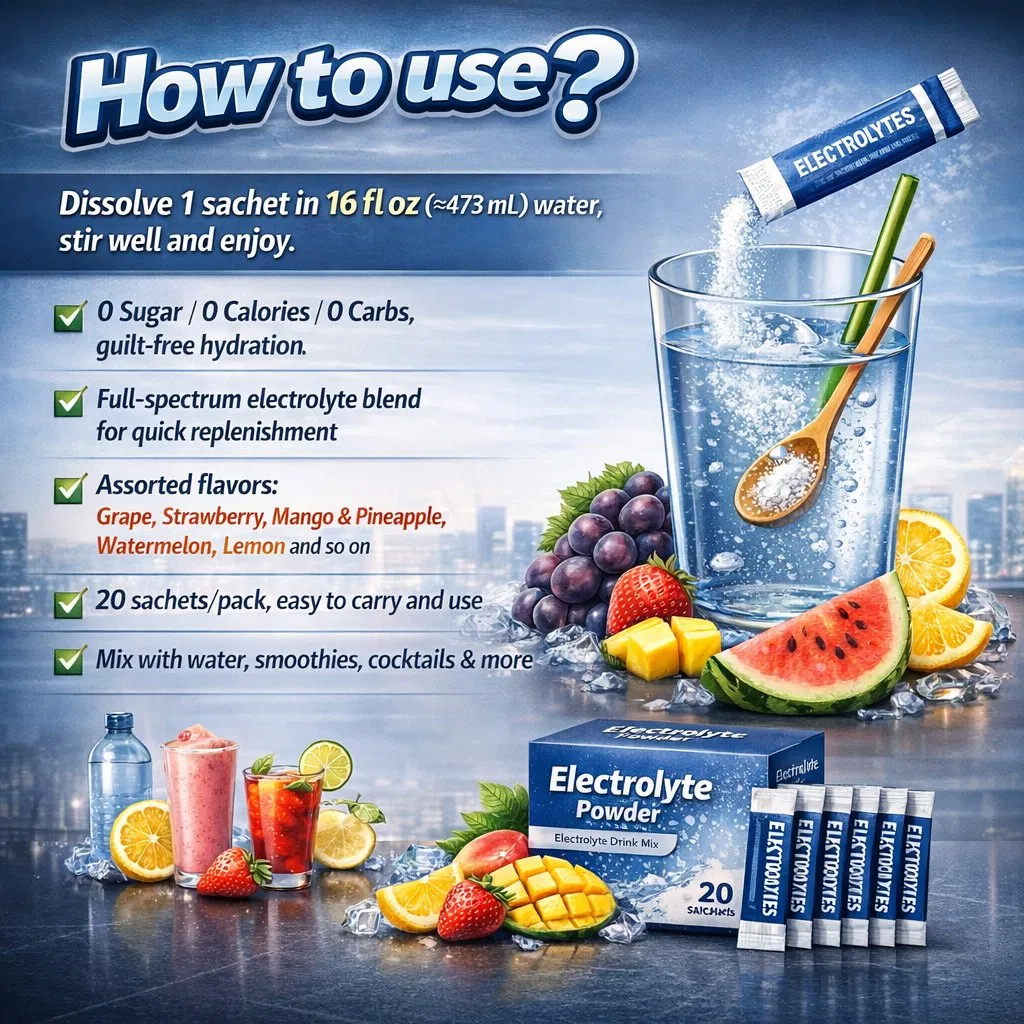
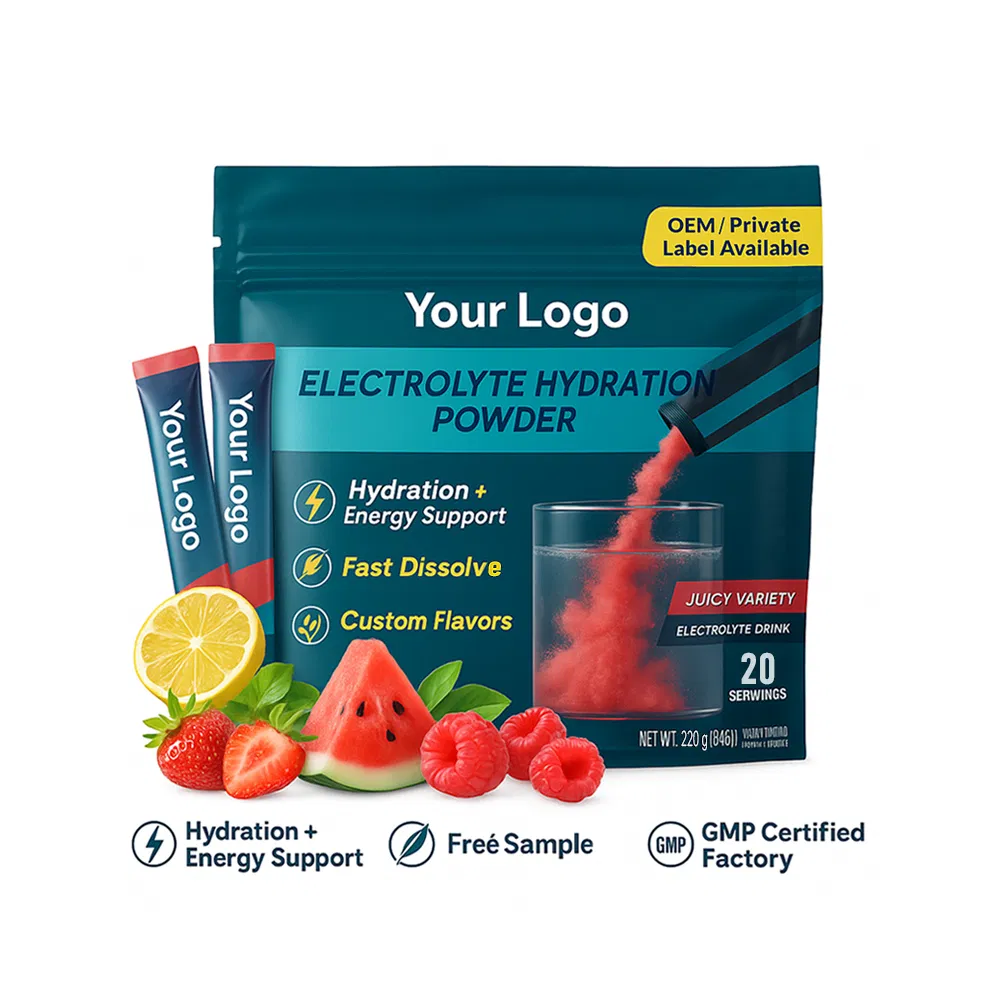
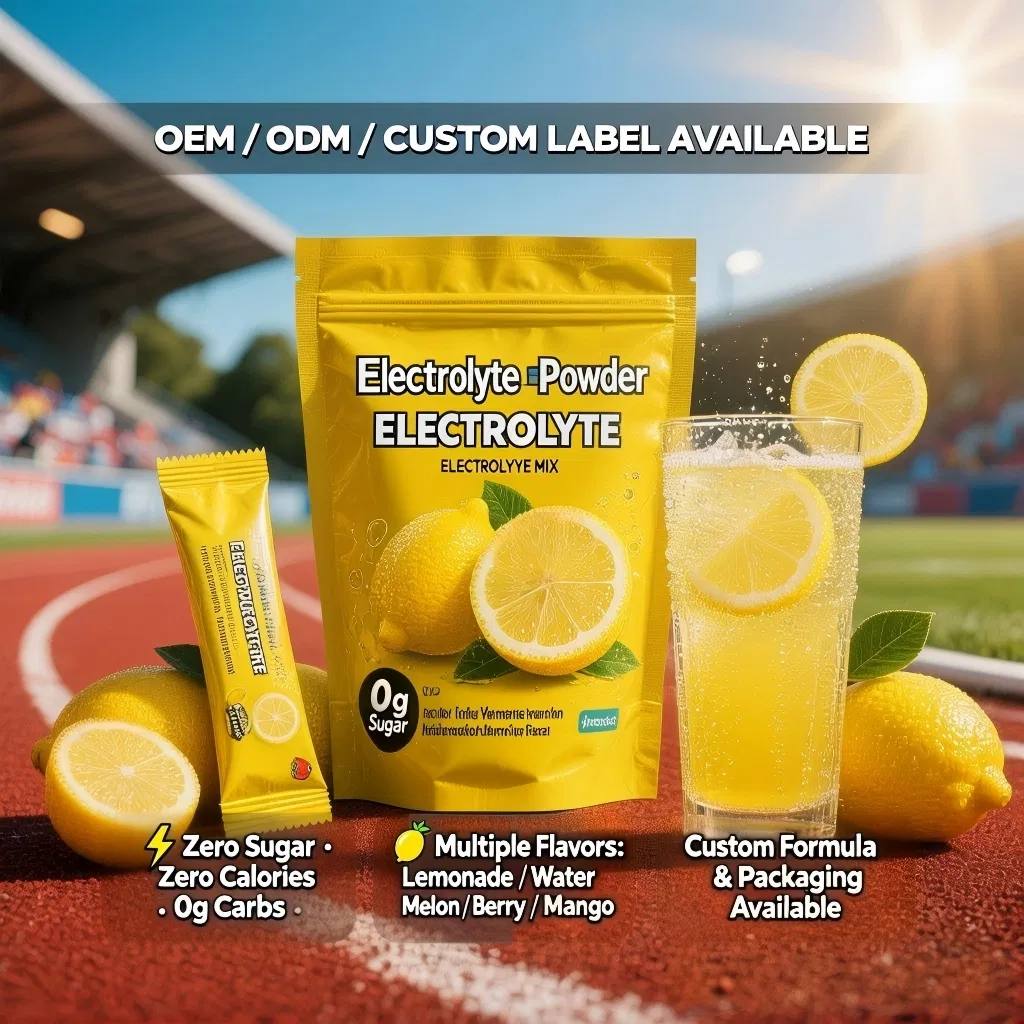
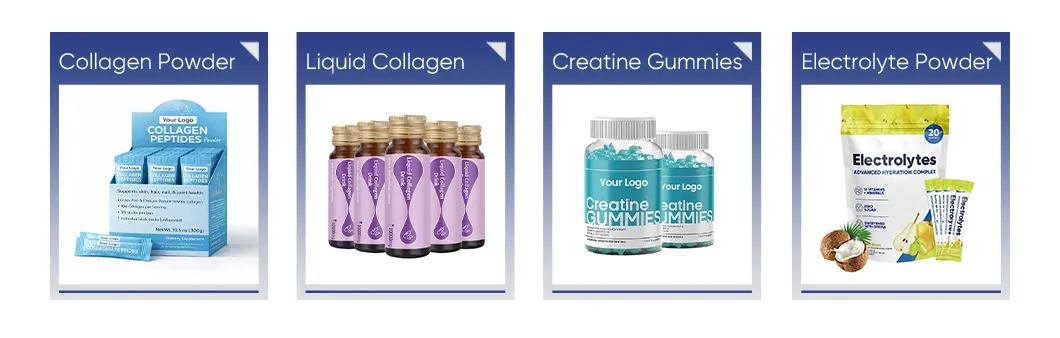
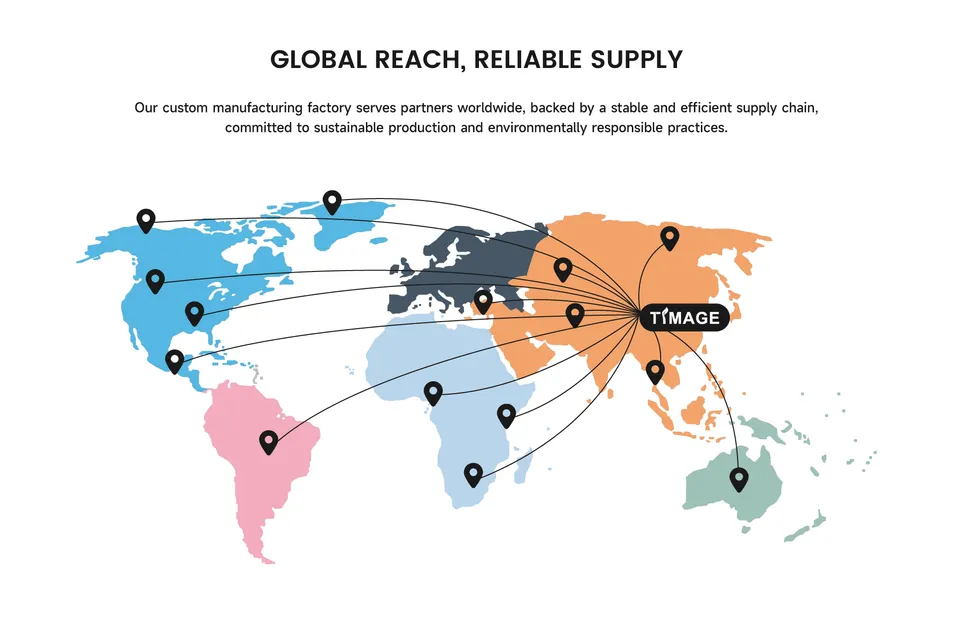
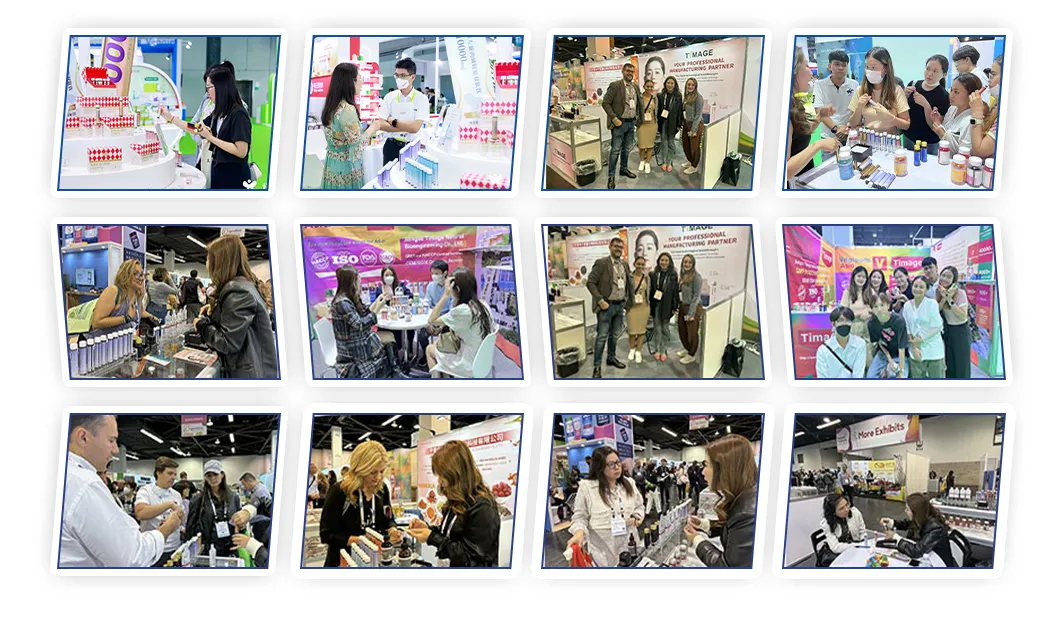
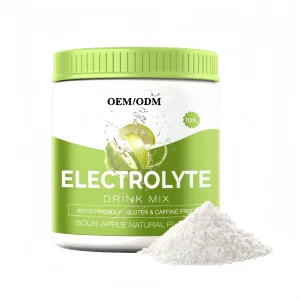
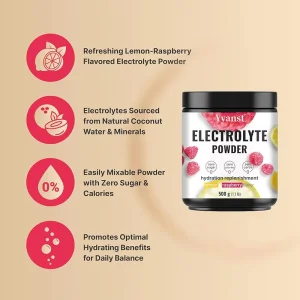
We leverage multiple health care production lines to achieve high annual output for electrolyte powder, collagen powder, creatine powder, fish oil, and melatonin tablet products, supporting both domestic sales and export business. With four years of export experience, we serve retailers, wholesalers, and private users across North America, Eastern Europe, Southeast Asia, the Middle East, Western Europe, and Northern Europe, while maintaining a strong presence in the domestic market.
Comprehensive after-sales support, flexible minimum order quantities above three hundred units, and stable material and packaging supply ensure reliable delivery for clients seeking long-term cooperation and continuous new product development. Recognized by IMDG CODE inspection reports, we demonstrate compliance with international safety standards and reinforce our reputation as a trusted bioengineering and health food manufacturer in global markets.
Q1. What certifications does the factory hold?
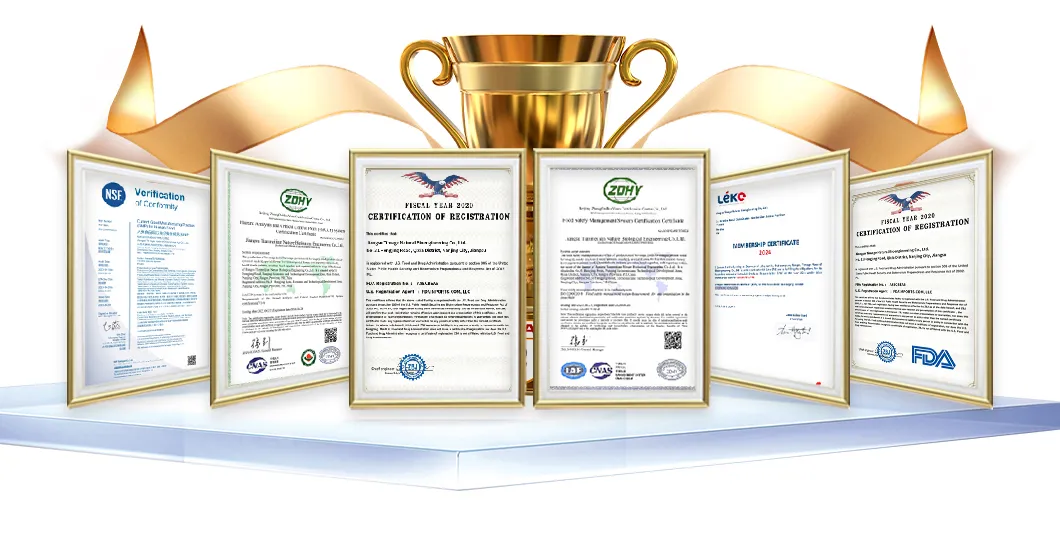
The factory and products are certified by GMP, HACCP, QS, and ISO.
Q2. Can I customize the logo and packaging?
Yes, we welcome customized logos and offer private label packaging options.
Q3. What is the minimum order quantity?
We support flexible MOQs and accept trial orders.
Q4. How long is the production lead time?
Lead time is within 7-15 working days for both peak and off-peak seasons.
Q5. Do you offer custom product development?
Yes, we can develop new products based on your special requirements or formulations.
Q6. What is the shelf life of the product?
The shelf life is 24 months when stored in a cool, dry, and dark location.
 Eik Health