Explore our custom OEM/ODM health solutions engineered for maximum nutrient delivery, stability, and market alignment.
Analyzing market vectors, CE certification protocols, and industrial-scale manufacturing requirements for global dietary supplements.
In the modern nutraceutical landscape, hydration is no longer viewed as merely the replacement of lost water. The biophysical dynamics of osmotic balance, intercellular fluid exchange, and metabolic recovery have turned hydration into a highly precise science. As sports performance, occupational health, and wellness consumerism reach new heights, CE certified electrolyte tablets have emerged as the gold standard for portable, stable, and highly bioavailable hydration.
Traditional ready-to-drink (RTD) electrolyte beverages are increasingly burdened by economic and environmental drawbacks, such as high shipping weights, excessive single-use plastic waste, and the need for chemical preservatives. In contrast, effervescent electrolyte tablets compress advanced active formulations into compact, anhydrous units. By delivering key minerals like sodium, potassium, magnesium, and calcium in a balanced effervescent carrier, these products maximize absorption via active cellular transport pathways, providing B2B buyers with a sustainable and high-margin product offering.
The global hydration supplement market is undergoing a paradigm shift driven by clean-label preferences, functional optimization, and sustainability. Consumers are moving away from legacy high-sugar sports drinks toward low-carb, zero-sugar electrolyte formulas that rely on natural sweeteners like stevia or monk fruit. This transition is especially evident in the athletic, wellness, and weight-management sectors, where glycemic impact is heavily scrutinized.
Moreover, there is an increasing demand for multi-functional electrolyte tablets. Today's formulas do not just focus on sodium-potassium ratios; they incorporate adaptogens, B-vitamins, branched-chain amino acids (BCAAs), and immune-supporting elements like Zinc and Vitamin C. As an experienced OEM/ODM partner, Guangdong Eik Health Co., Ltd. continuously monitors these consumer preferences to help brands develop forward-looking formulations that satisfy the modern consumer's demand for clean, effective ingredients.
For global enterprise buyers, navigating the regulatory environment of different target markets is the biggest hurdle to product expansion. The CE (Conformité Européenne) marking indicates that a product complies with the essential health, safety, and environmental protection standards of the European Economic Area (EEA). In the context of dietary supplements and effervescent delivery formats, CE certification serves as a seal of quality that guarantees compliance with strict EU safety directives.
Achieving CE compliance requires strict validation of the raw materials, manufacturing practices, stability data, and packaging integrity. Every batch of electrolyte tablets must fall within precise tolerance levels for heavy metals, microbial counts, and active compound variance. This regulatory security provides major brands, retail distributors, and clinical procurement agents with the absolute confidence that their imported supplements will pass customs smoothly and perform safely in the hands of the end consumer.
Large-scale B2B buyers—ranging from multinational retail networks to military suppliers and industrial safety organizations—have procurement guidelines that go far beyond basic wholesale requirements. Enterprise procurement prioritizes three main pillars:
Guangdong Eik Health Co., Ltd. sits at the intersection of advanced manufacturing technology and global logistical convenience. Operating out of China's primary industrial innovation corridor, our facility leverages automated manufacturing frameworks (Industry 4.0 standards) to achieve unmatched production speed, consistent tablet density, and excellent cost efficiency.
Our factory features clean-room environments with strict relative humidity (RH) control of under 20%—a critical requirement for stable effervescent compression. By automating material feed, blending, high-speed tableting, and immediate barrier sealing, we minimize environmental exposure and eliminate batch-to-batch variation.
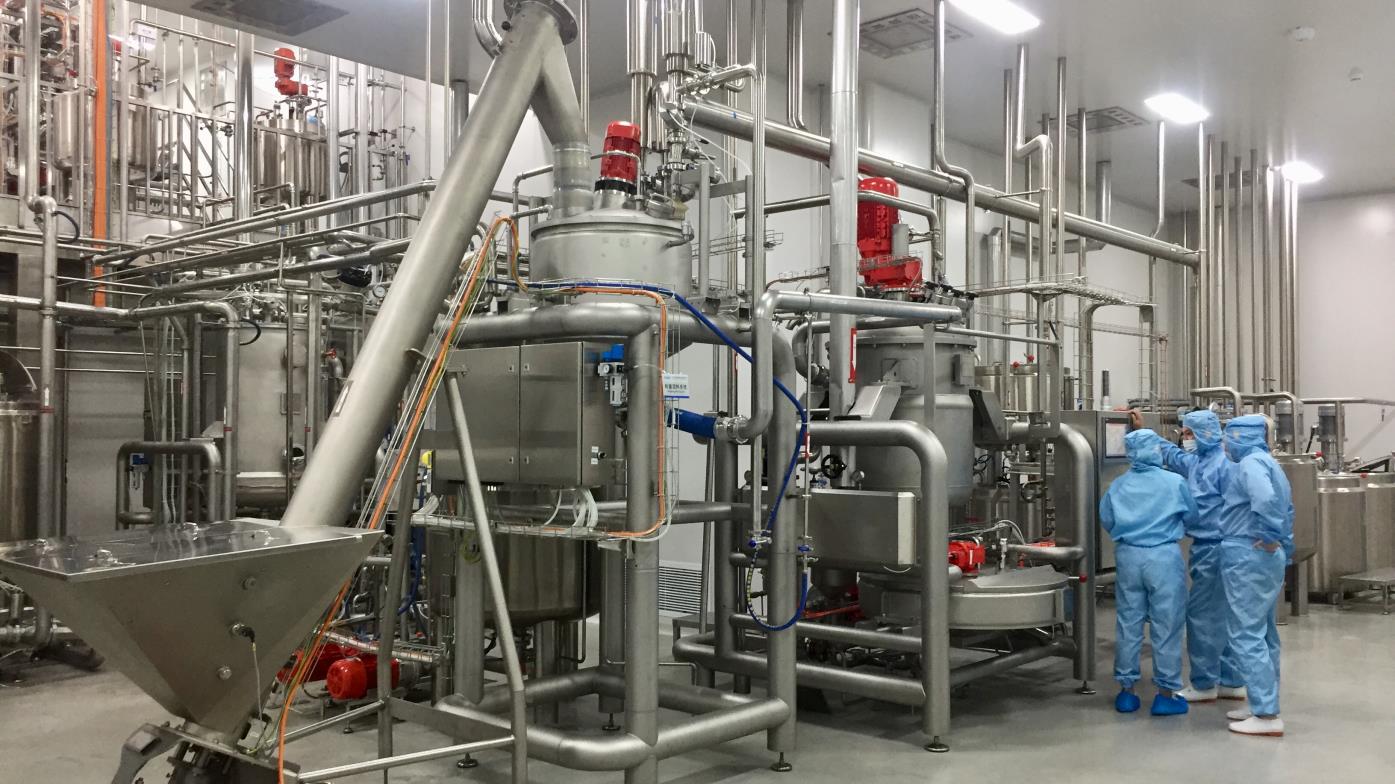
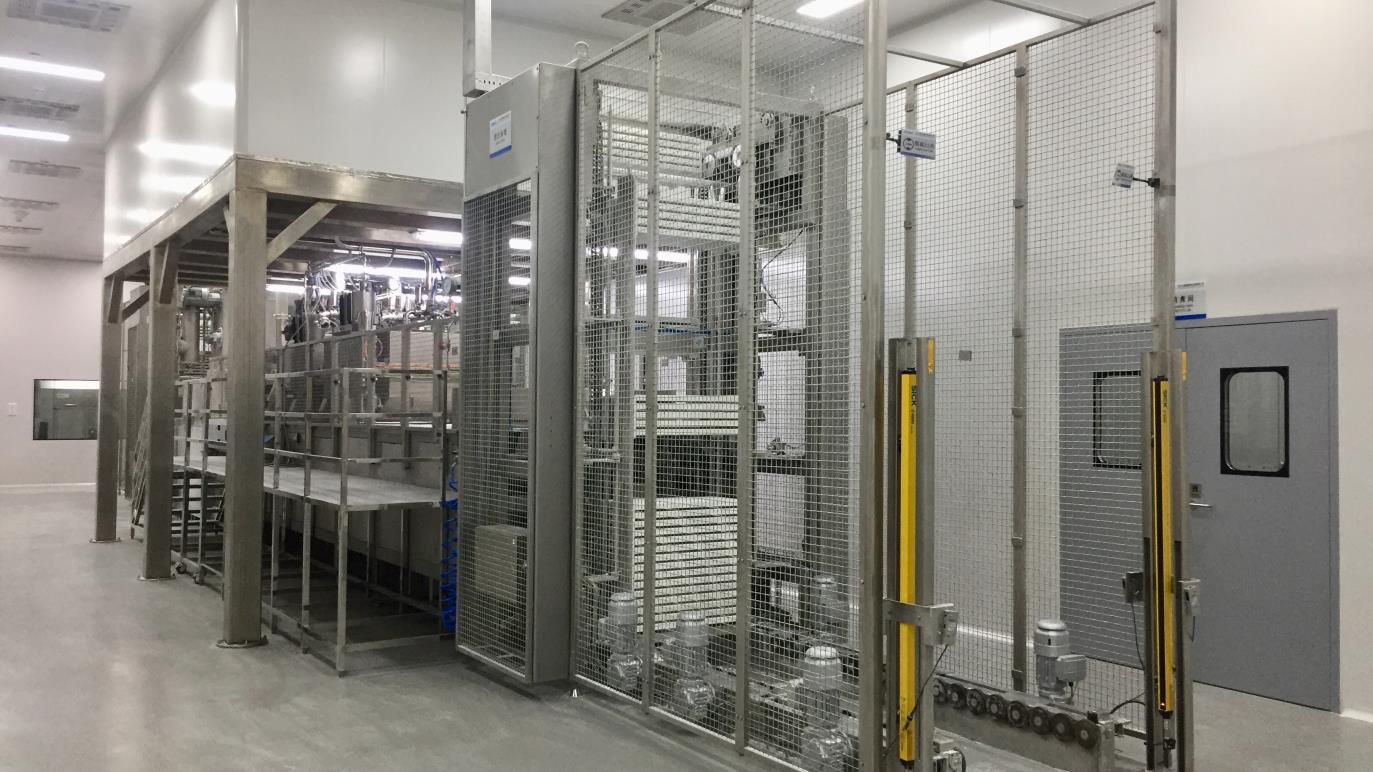
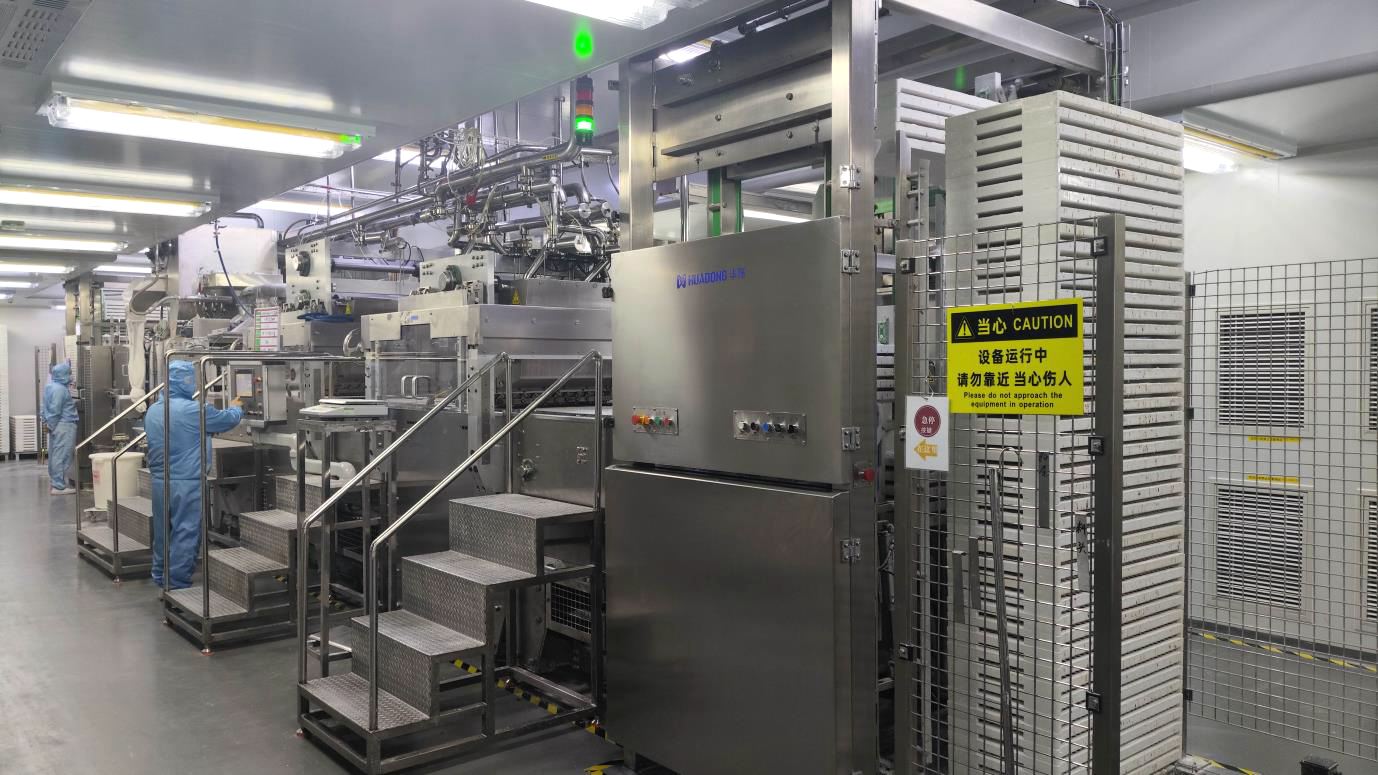
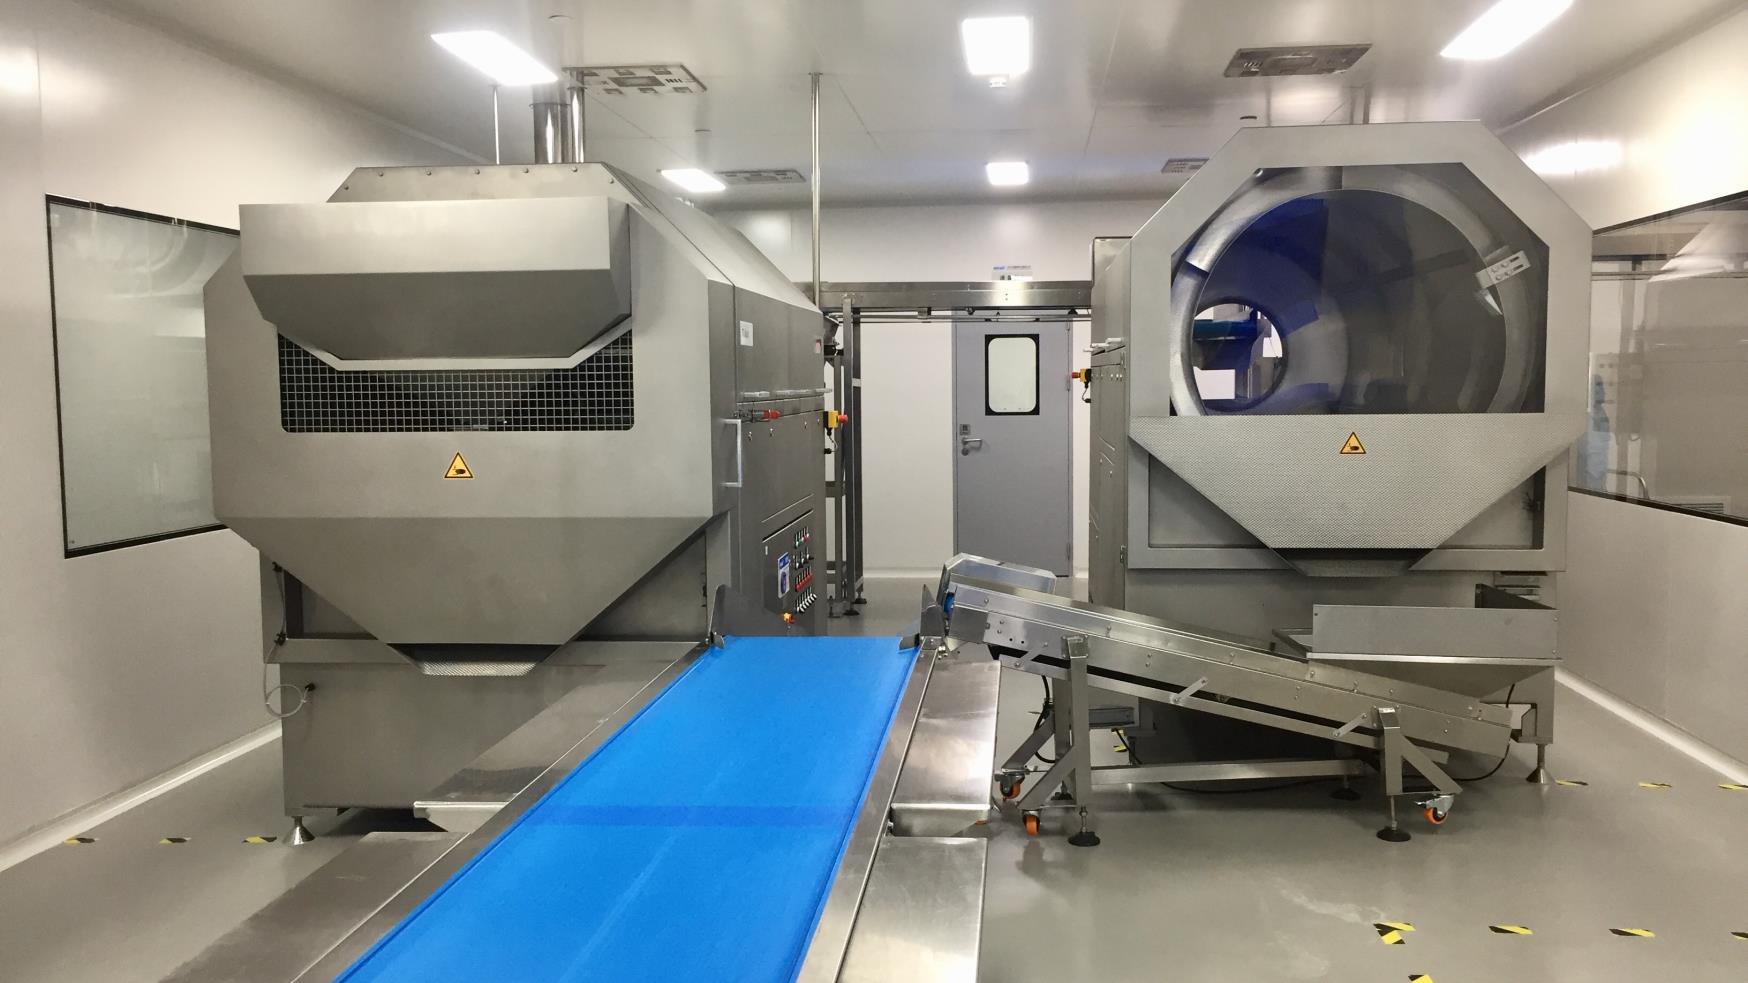
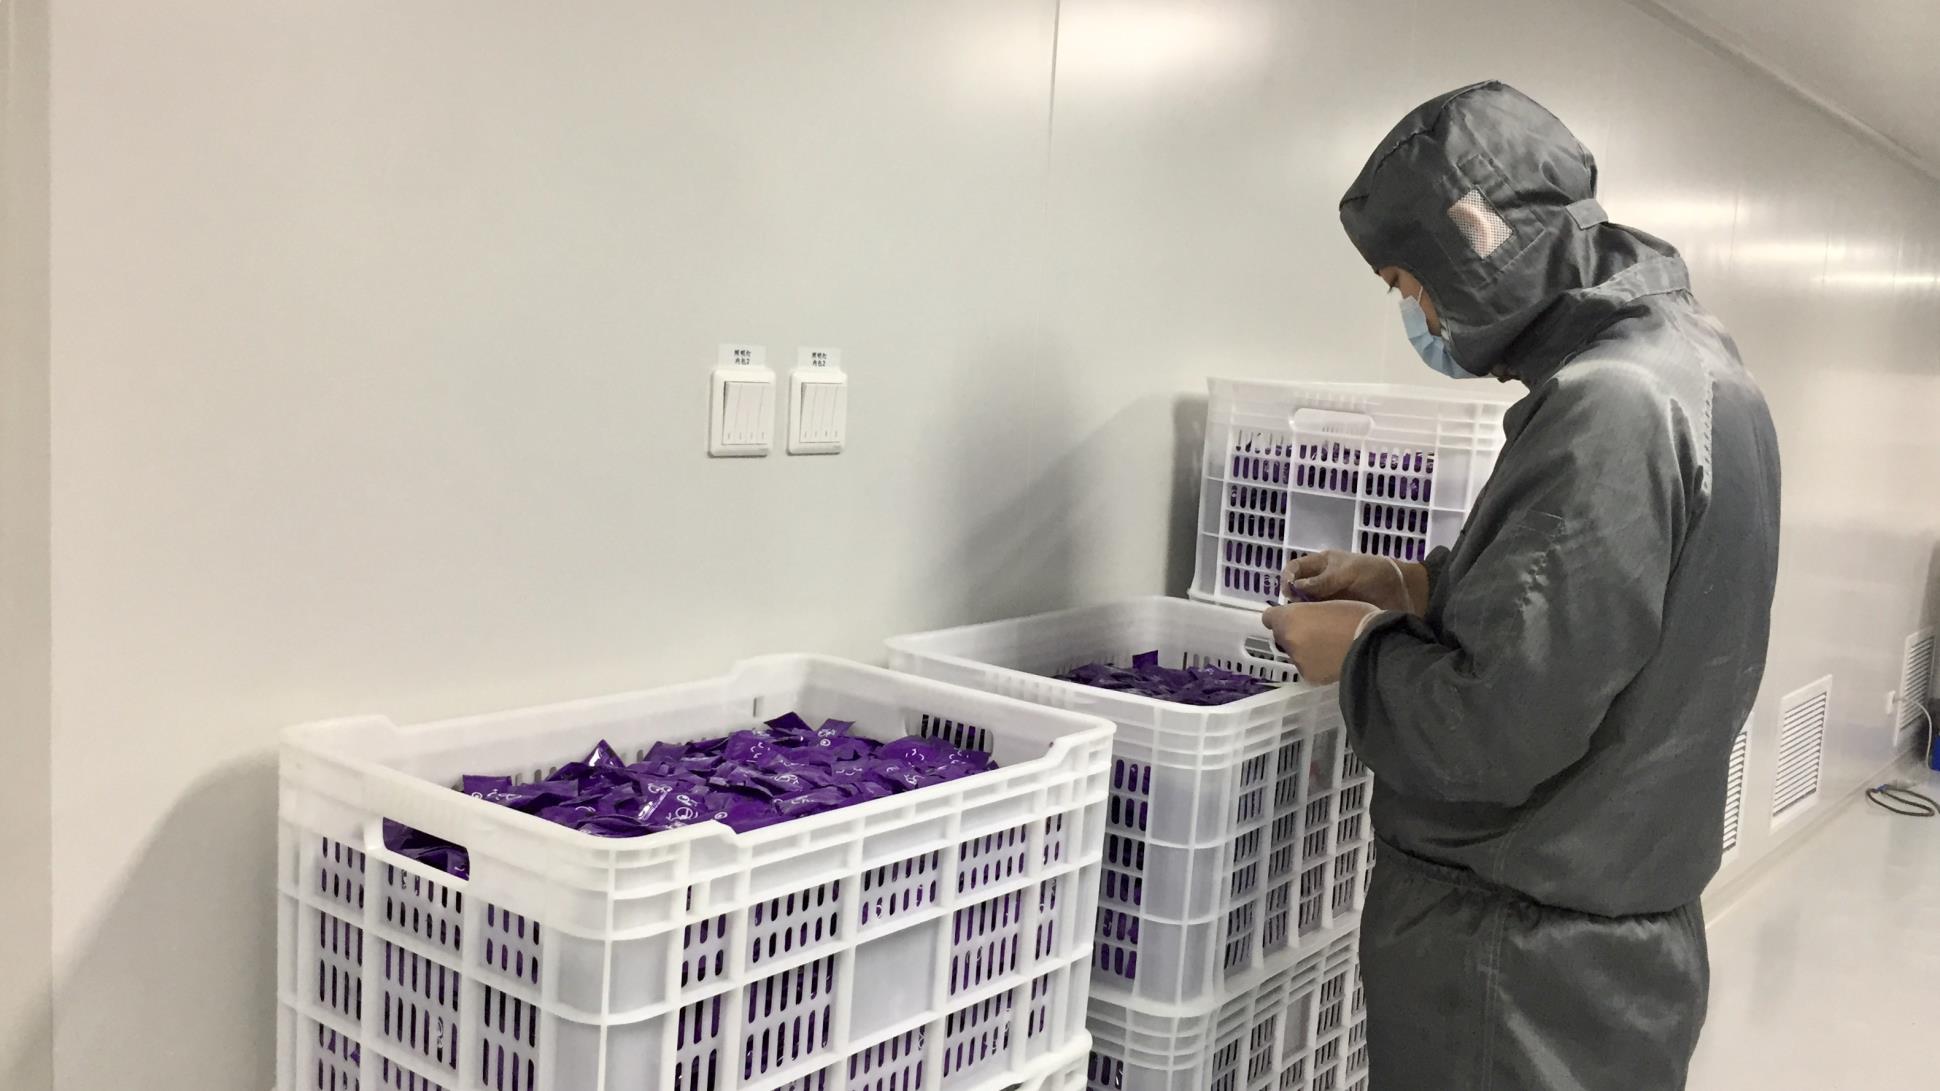
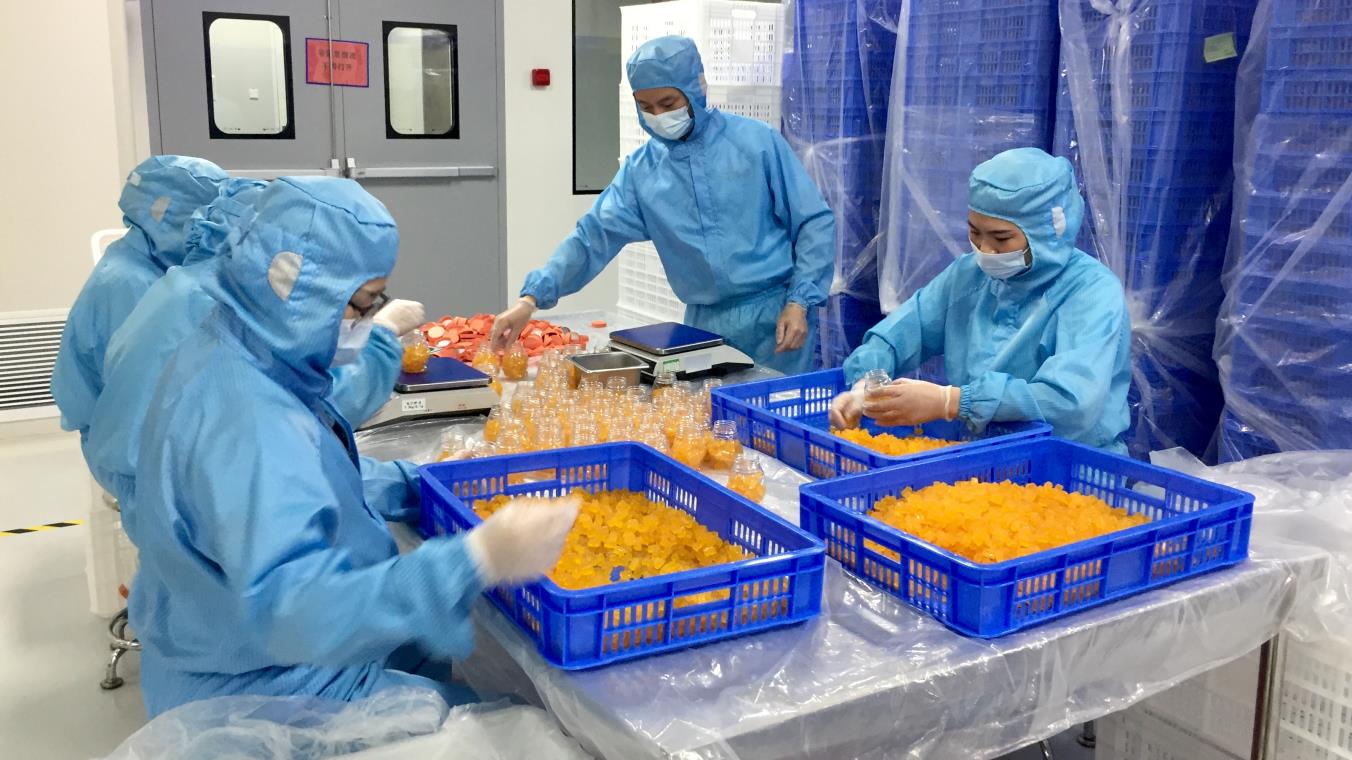
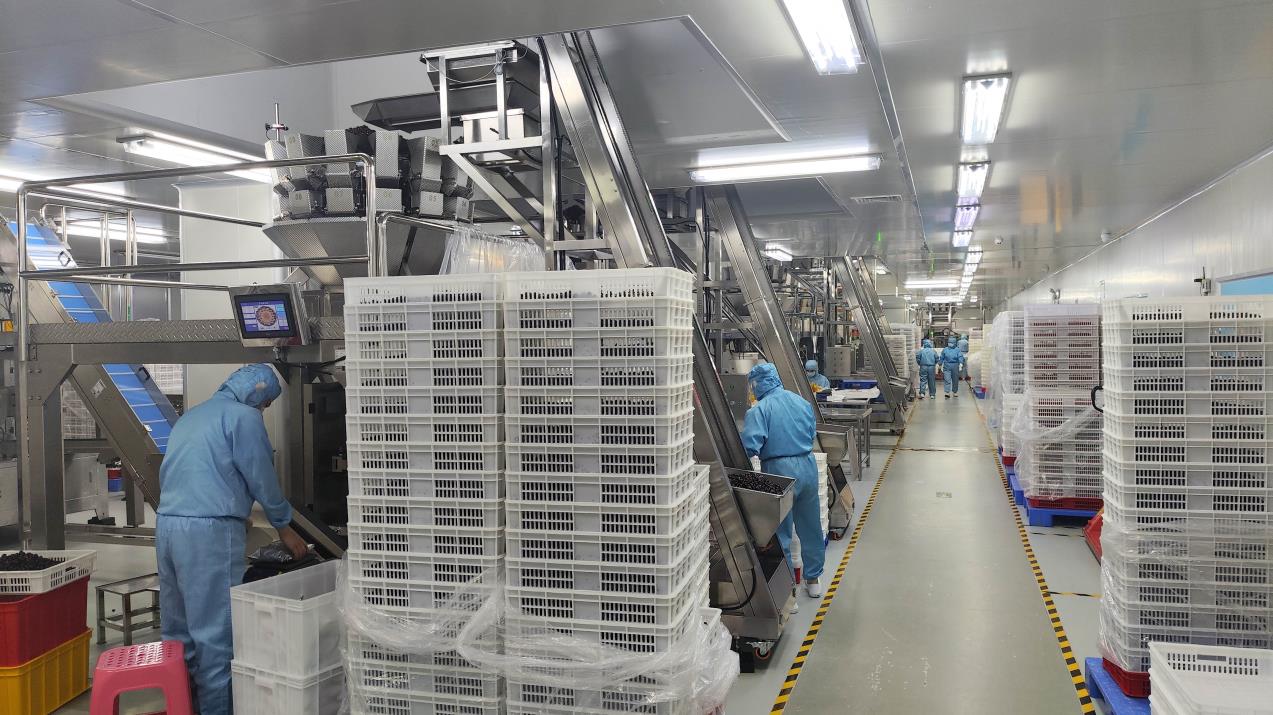
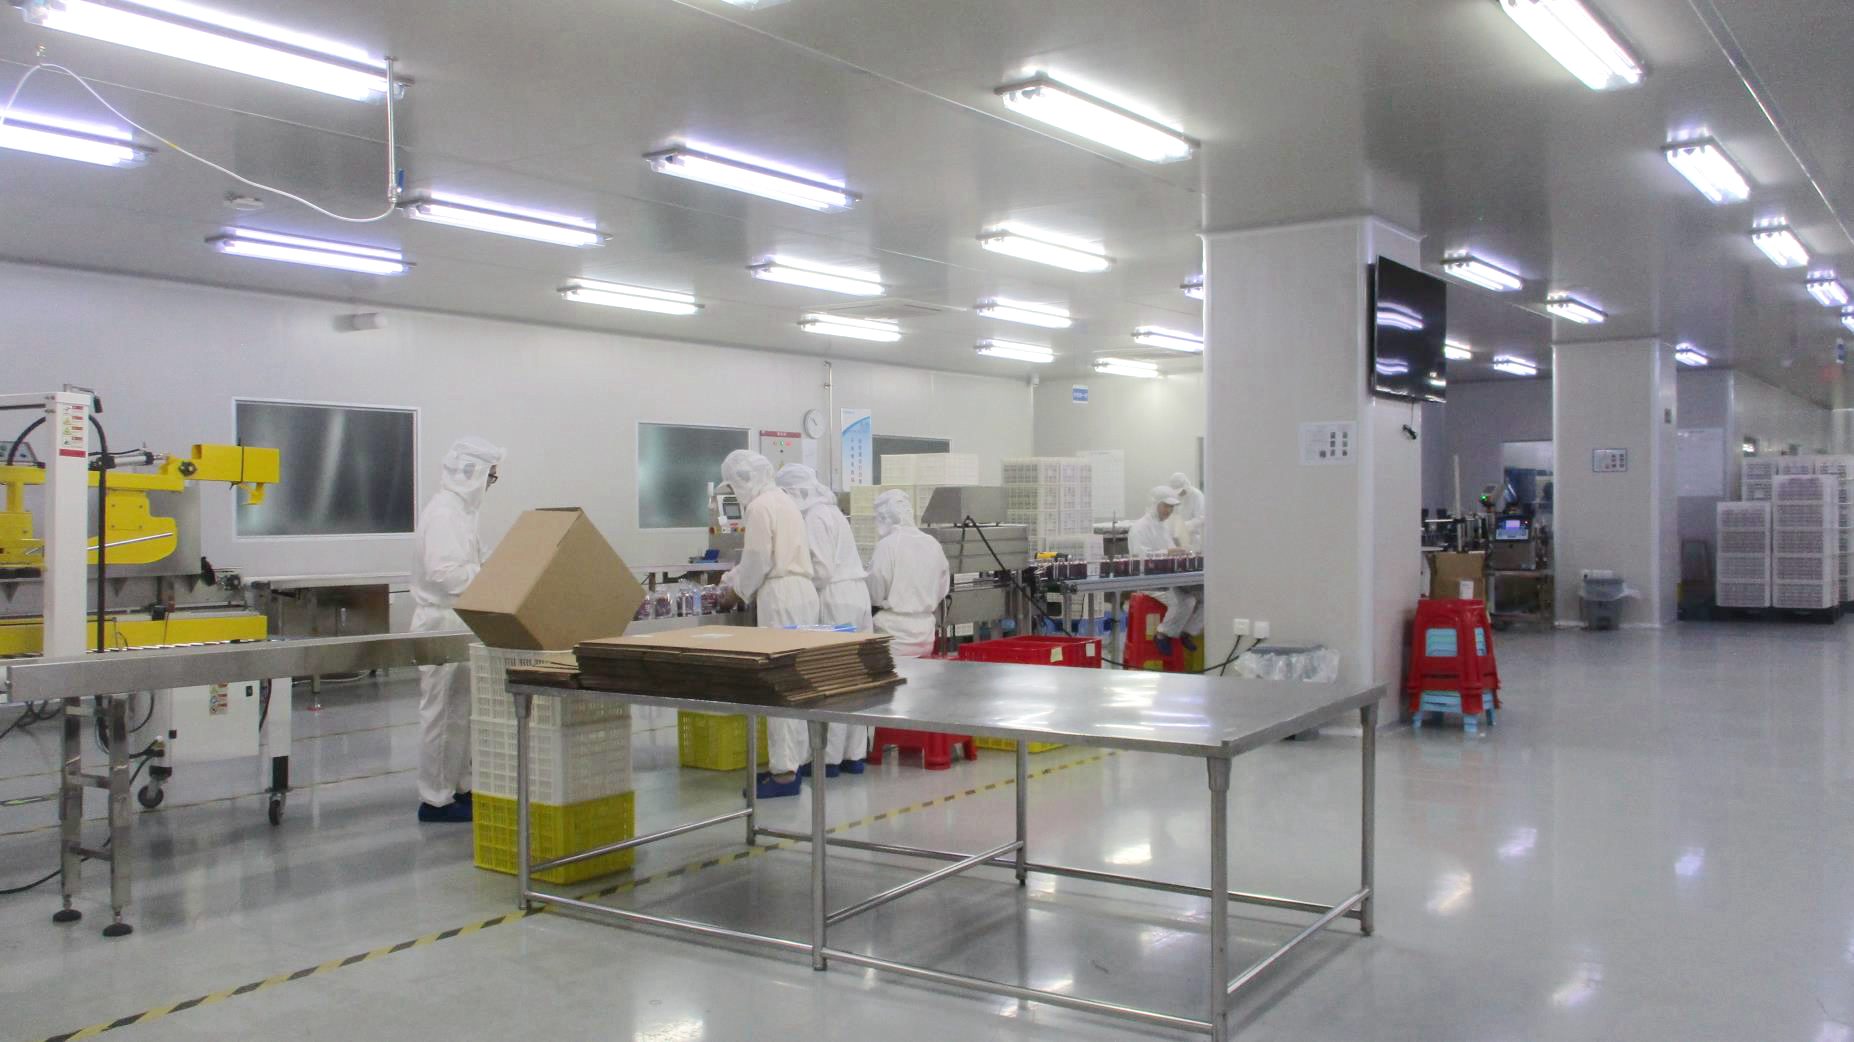
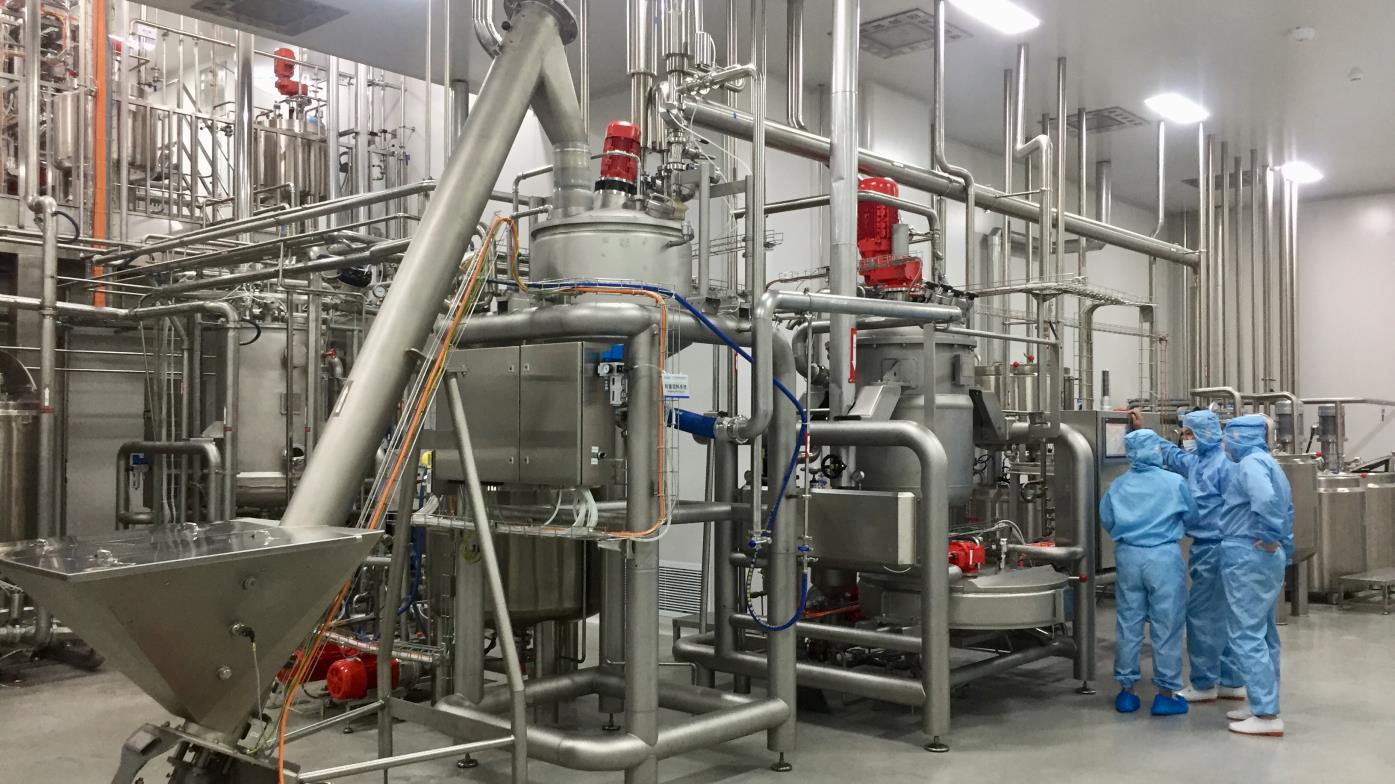
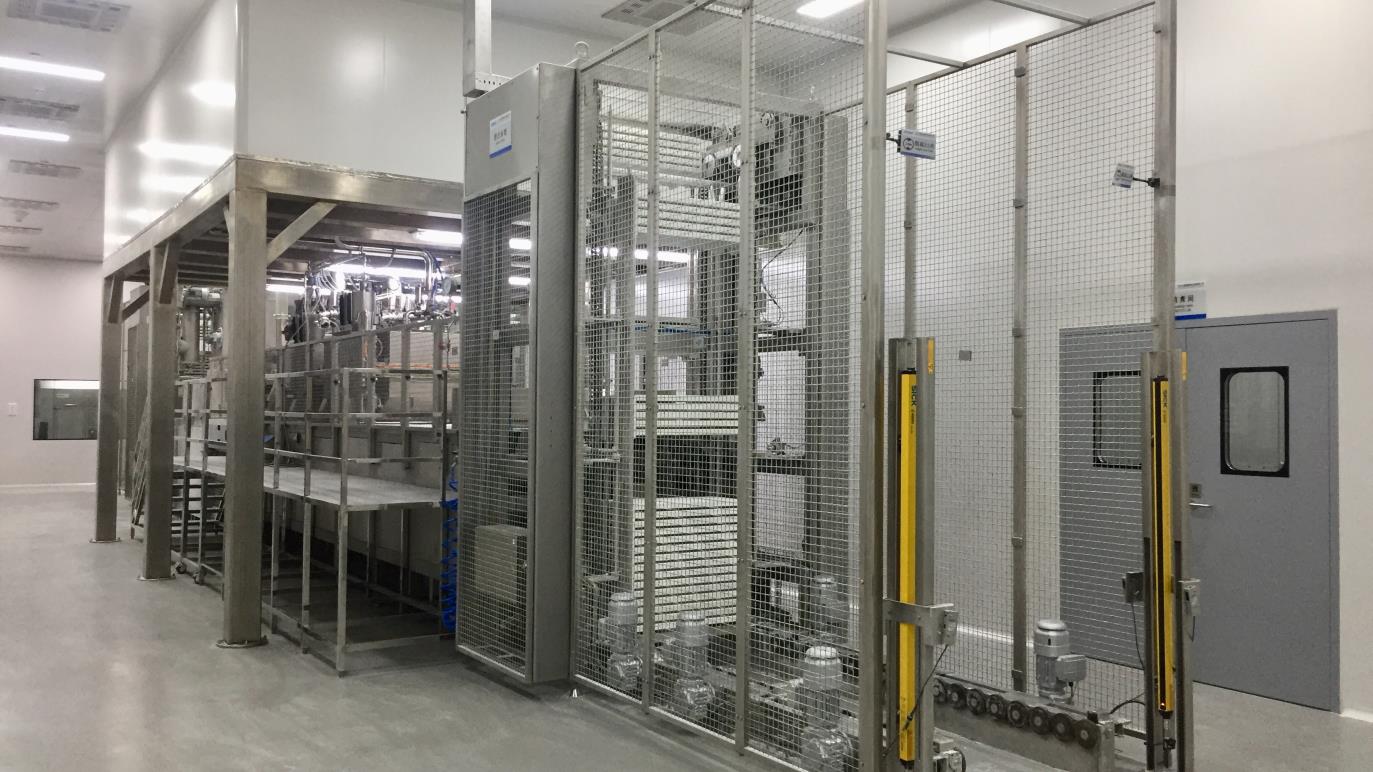
As described in the workflow above, our manufacturing infrastructure utilizes specialized, industrial-scale lines—including our Boiling Production Line and Pouring Production Line—to ensure high-precision material blending and tablet integrity. Each step of the process, from molding and polishing to meticulous quality control (QC) checks, is monitored by our QA engineers to maintain zero defect rates.
Electrolyte tablets are highly versatile products serving many different markets and demographics. By varying the active concentrations, flavors, and packaging styles, brands can position these tablets for several unique application scenarios:
Formulated for endurance runners, cyclists, and team sports. These tablets focus on rapid muscle cramp prevention and ATP regeneration, featuring high concentrations of magnesium citrate, sodium chloride, and potassium along with added L-glutamine and BCAAs.
Designed for heavy labor in high-heat environments. These formulations are designed to prevent heat fatigue and maintain cognitive function over long shifts. They are typically packaged in cost-effective bulk strip packs for corporate safety procurement.
Focused on rapid physiological rehydration following dehydration, illness, or alcohol consumption. These tablets utilize exact sodium-to-glucose ratios to activate the sodium-glucose cotransport mechanism in the small intestine for incredibly fast fluid absorption.
Aimed at health-conscious consumers and individuals following ketogenic diets. Formulated with zero sugar, natural flavors, and organic colorants, these tablets provide clean hydration and help prevent mineral deficiencies during fasting or carb restriction.
Guangdong Eik Health Co., Ltd. is a professional China-based manufacturer specializing in OEM and ODM nutritional supplement solutions. With extensive experience in the health and nutrition industry, we are dedicated to providing global customers with reliable, flexible, and high-quality supplement manufacturing services.
We offer comprehensive solutions covering product development, customized formulation, ingredient sourcing, production, packaging, and private label services. Our manufacturing capabilities include gummies, capsules, softgels, tablets, powders, liquids, and other customized nutritional products, helping brands efficiently transform innovative ideas into market-ready health solutions.
Equipped with modern production facilities, advanced manufacturing equipment, and a strict quality management system, Guangdong Eik Health ensures consistent product quality and safety throughout the manufacturing process. We work with a wide range of premium raw materials and have access to more than 1,000 functional ingredients, enabling us to create customized supplement formulas that meet different market demands and consumer preferences.
With an efficient supply chain system and strong production capacity, we provide competitive solutions with flexible order quantities, fast quotation services within 24–48 hours, and optimized production schedules. Depending on product specifications and order requirements, our lead times can start from approximately 15 days, helping customers respond quickly to market opportunities.
Discover our broader selection of functional powders, target support supplements, and advanced enzyme formulations.
 Eik Health